Description
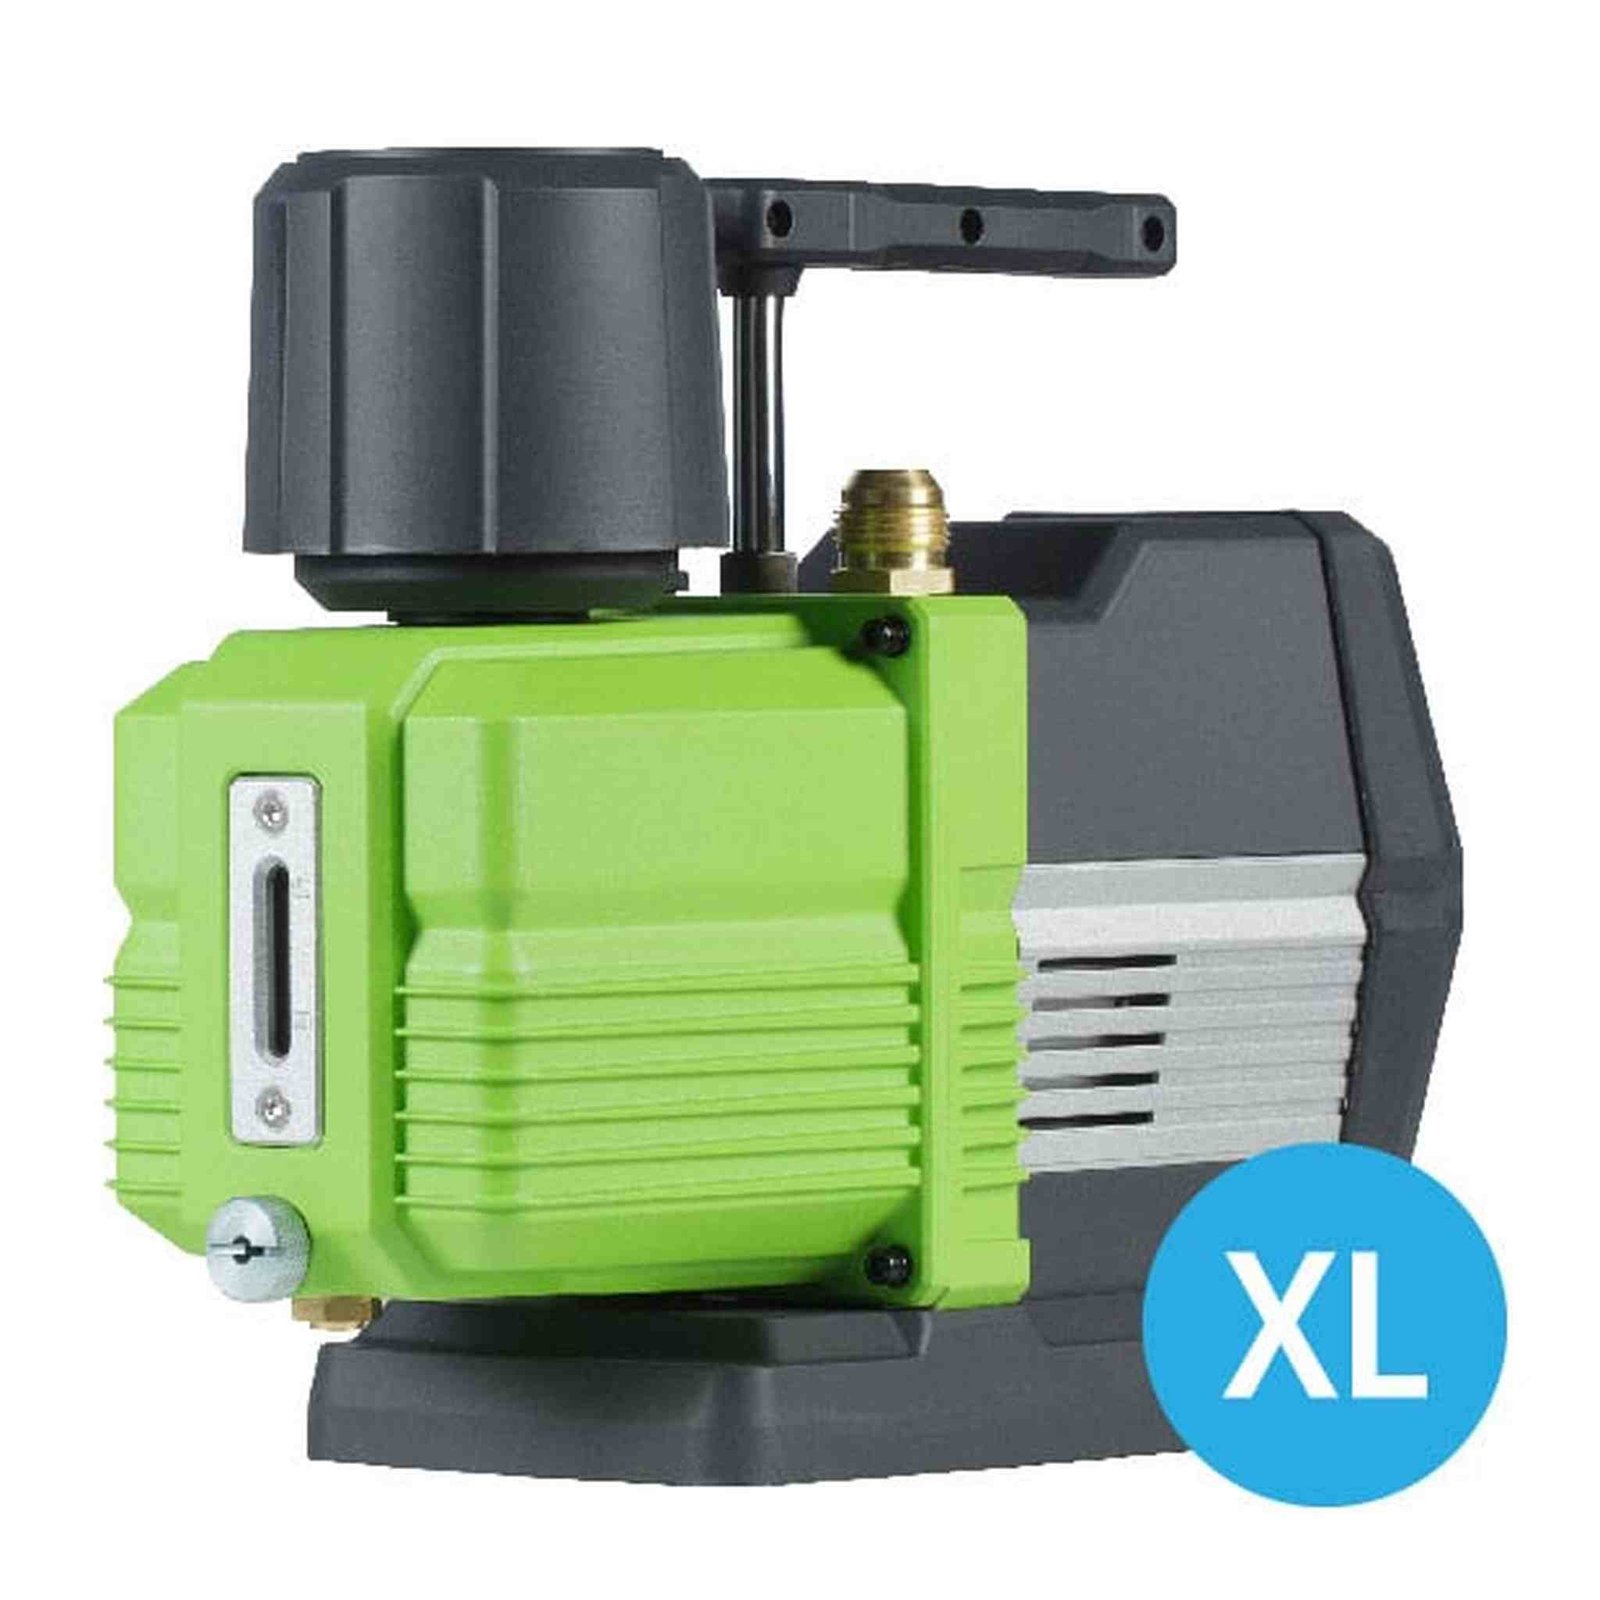
Harvest Right XL Premier Industrial Vacuum Pump – 110V Oil Pump for High-Capacity Freeze Drying
ESTIMATED DELIVERY TIME FOR ALL HARVESTRIGHT PRODUCTS IS 2–3 WEEKS
Unlock industrial-grade vacuum performance with the Harvest Right XL Premier Industrial Vacuum Oil Pump (110V)—a powerhouse solution engineered for X-Large and commercial freeze-drying systems. Built for demanding, high-volume operations, this oil pump combines deep vacuum strength, quiet operation, and long-lasting durability to optimize your freeze-drying throughput.
Ideal for commercial kitchens, laboratories, and professional food preservation setups, this pump ensures rapid cycles and extended reliability with minimal maintenance.
Key Features – XL Premier Industrial Vacuum Oil Pump 110V
-
Heavy-Duty Vacuum Power
Delivers strong, consistent suction ideal for large-capacity and commercial Harvest Right Freeze Dryers. -
Low-Noise Operation
Runs at just 52 decibels—perfect for quiet lab environments and commercial production facilities. -
Longer Oil Life
Features an oversized oil reservoir and advanced filtration system for fewer oil changes and less downtime. -
Built to Last
Heavy-duty motor and high-precision components ensure reliable performance under continuous operation. -
Faster Freeze-Drying Cycles
Powerful vacuum reduces drying times, increasing productivity for large batch processing. -
User-Friendly Maintenance
Equipped with an oil sight glass and easy-access drain valve for quick, clean oil changes. -
Easy Integration
Includes hose and fittings for seamless plug-and-play setup with your Harvest Right Freeze Dryer. -
Energy Efficient Design
Optimized for performance without unnecessary power consumption.
Specification
Technical Specifications
Oil: Robinair Premium High Vacuum Pump Oil or JB Industries Black Gold Vacuum Pump Oil Only
DC Motor
Energy Efficient
Voltage: Standard, 115v, 60Hz
Dimensions: 16.3″ x 6″ x 12.1″
Weight: 35lbs